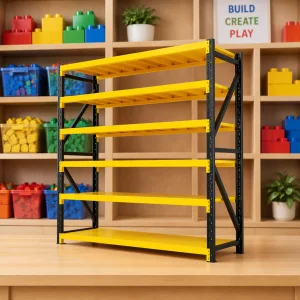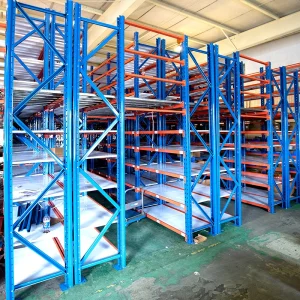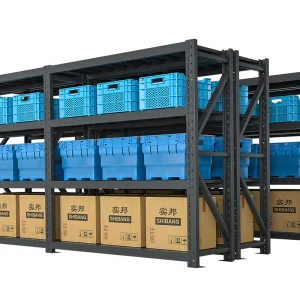
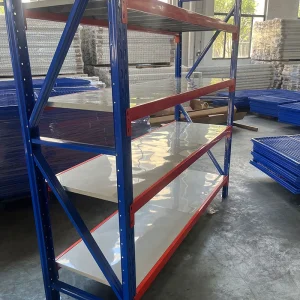
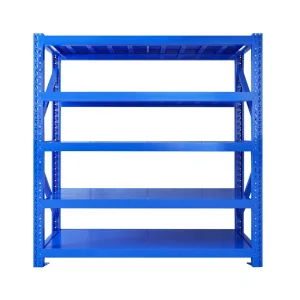
Established in 2016, Ningbo Shibang Storage Rack Co., Ltd. is a leading enterprise specializing in the design, manufacture, and global distribution of heavy-duty industrial warehouse racking systems. Spanning a modern manufacturing facility of 32,000 m², our company has accumulated 12 years of industry experience and 8 years of direct export expertise, serving global clients with total annual export revenue reaching $18 million.
Quality and structural integrity are at the core of our manufacturing philosophy. Backed by a dedicated quality control team of 35 QA/QC inspectors, we implement rigorous multi-stage quality assurance processes, including Ultrasonic Testing (UT) for weld seams, load-bearing stress analysis, coating thickness verification, and raw material tensile testing.
Advanced Facility
QA/QC Experts
Annual Revenue
Supply Partners
Operating with a robust international trade setup, our primary markets cover North America, Western Europe, Southeast Asia, and Australia. To maintain efficient production cycles and reliable raw material supply, we partner with over 850 supply chain vendors. Our diverse client portfolio spans 3PL logistics providers, automated distribution centers, retail mega-warehouses, and heavy manufacturing facilities.
Innovation drives our growth. Our in-house R&D department boasts 22 experienced structural and mechanical engineers. Through strong technical capability and advanced OEM/ODM versatility, we offer extensive customization options, including tailored load capacities, custom powder-coating colors, seismically engineered beam profiles, and modular height configurations. Demonstrating our commitment to evolving market needs, we launched 140 new products and optimized structural components over the past year alone.
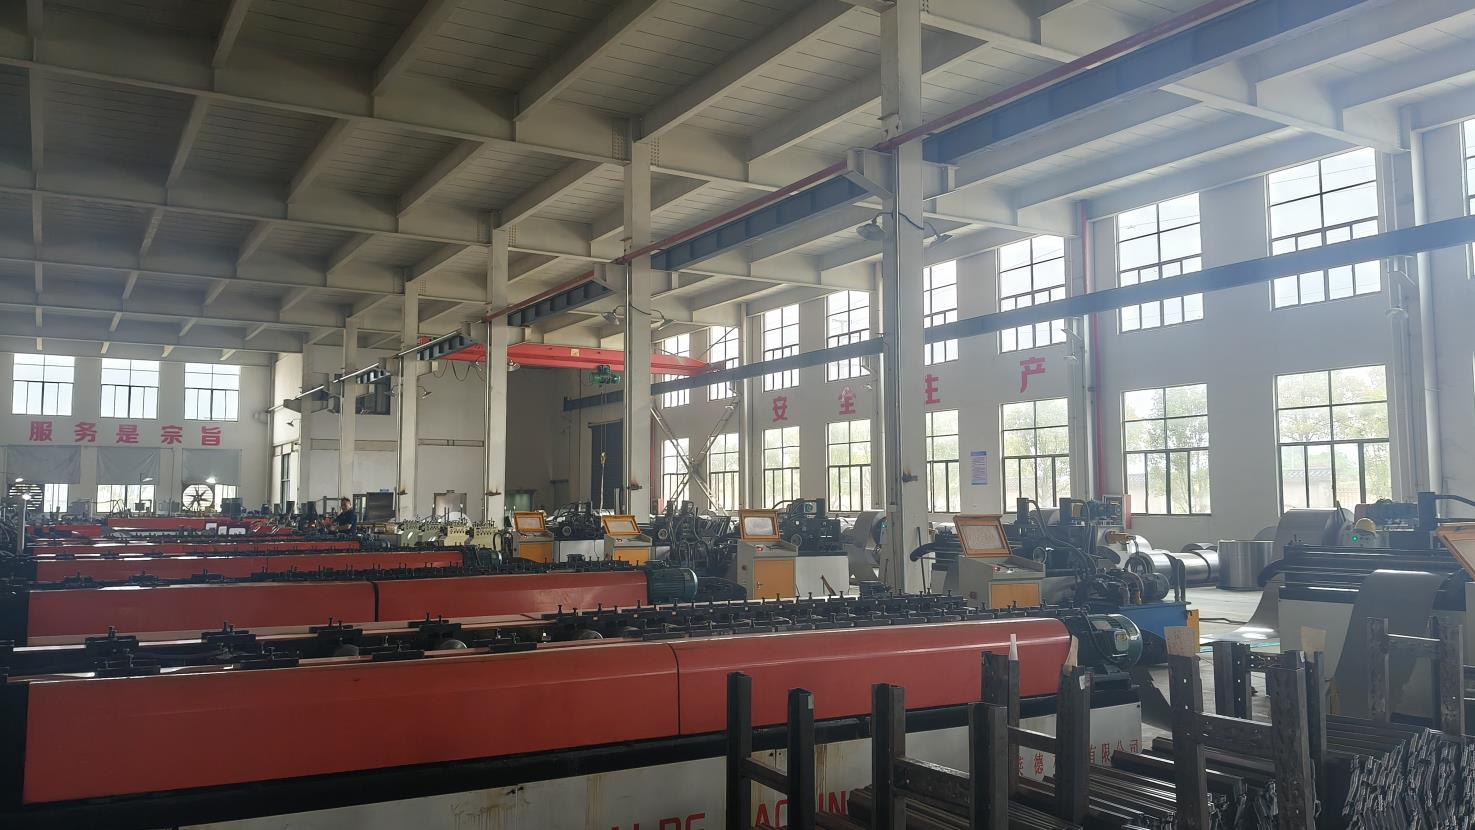
Forming
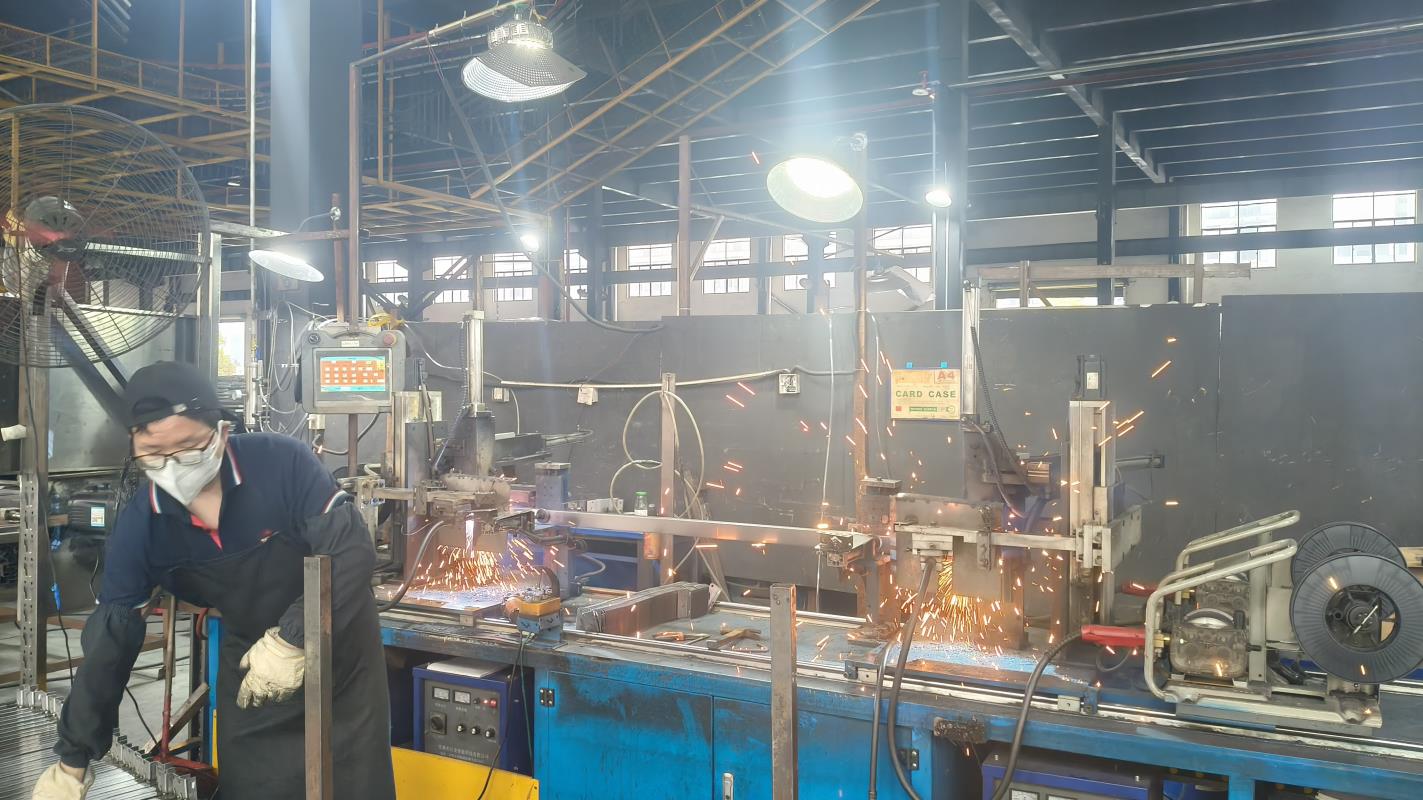
Bonding
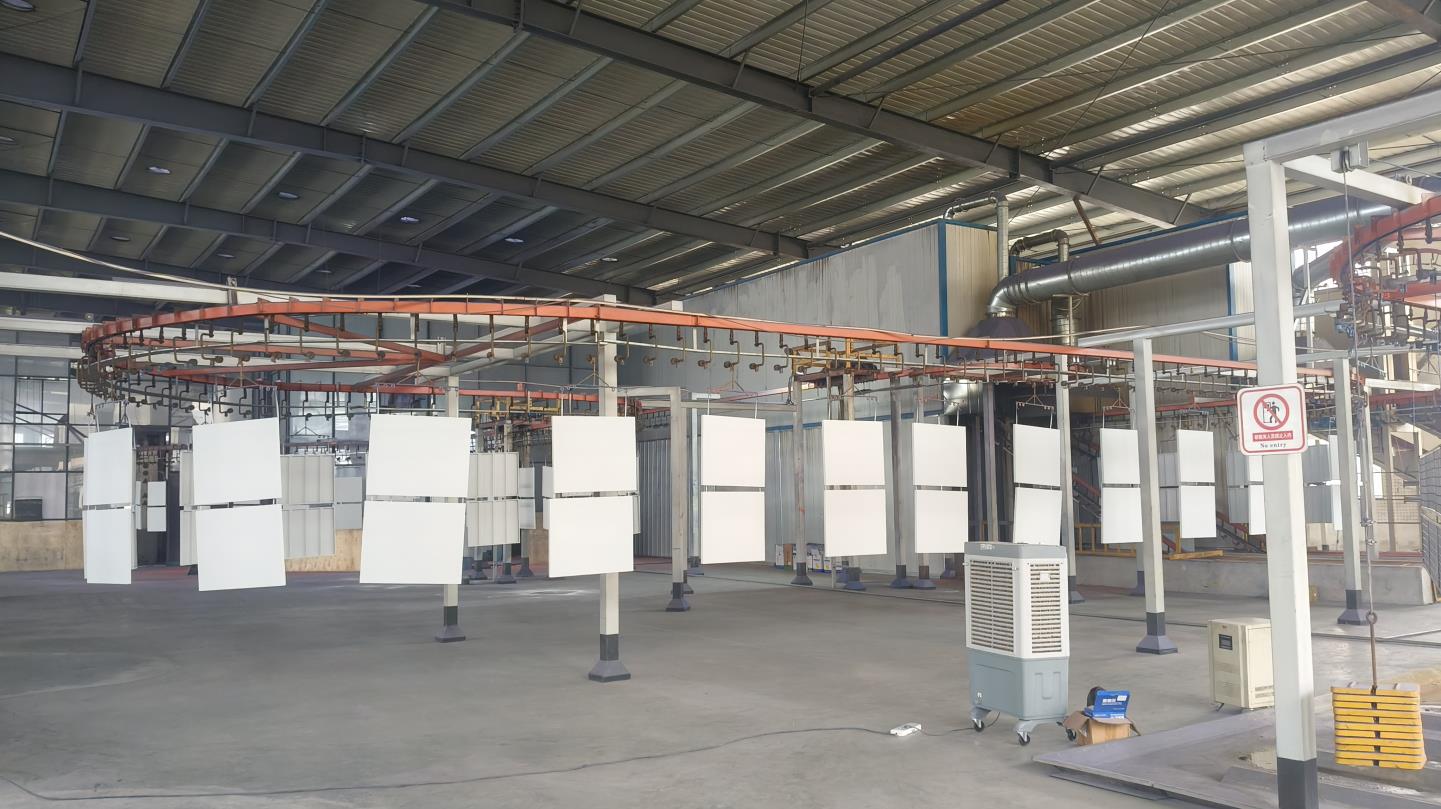
Spray painting
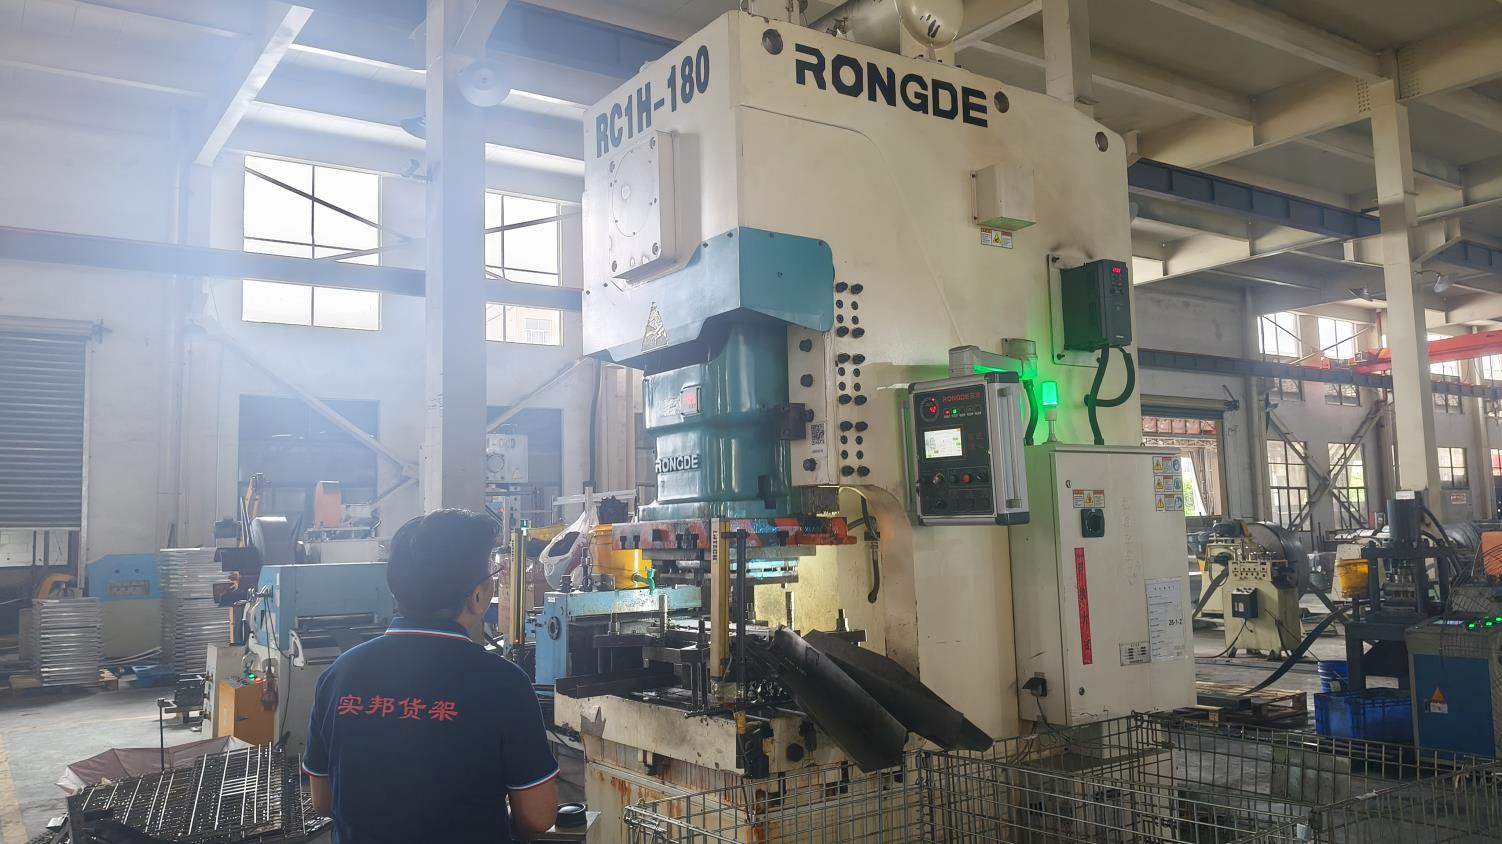
Punching
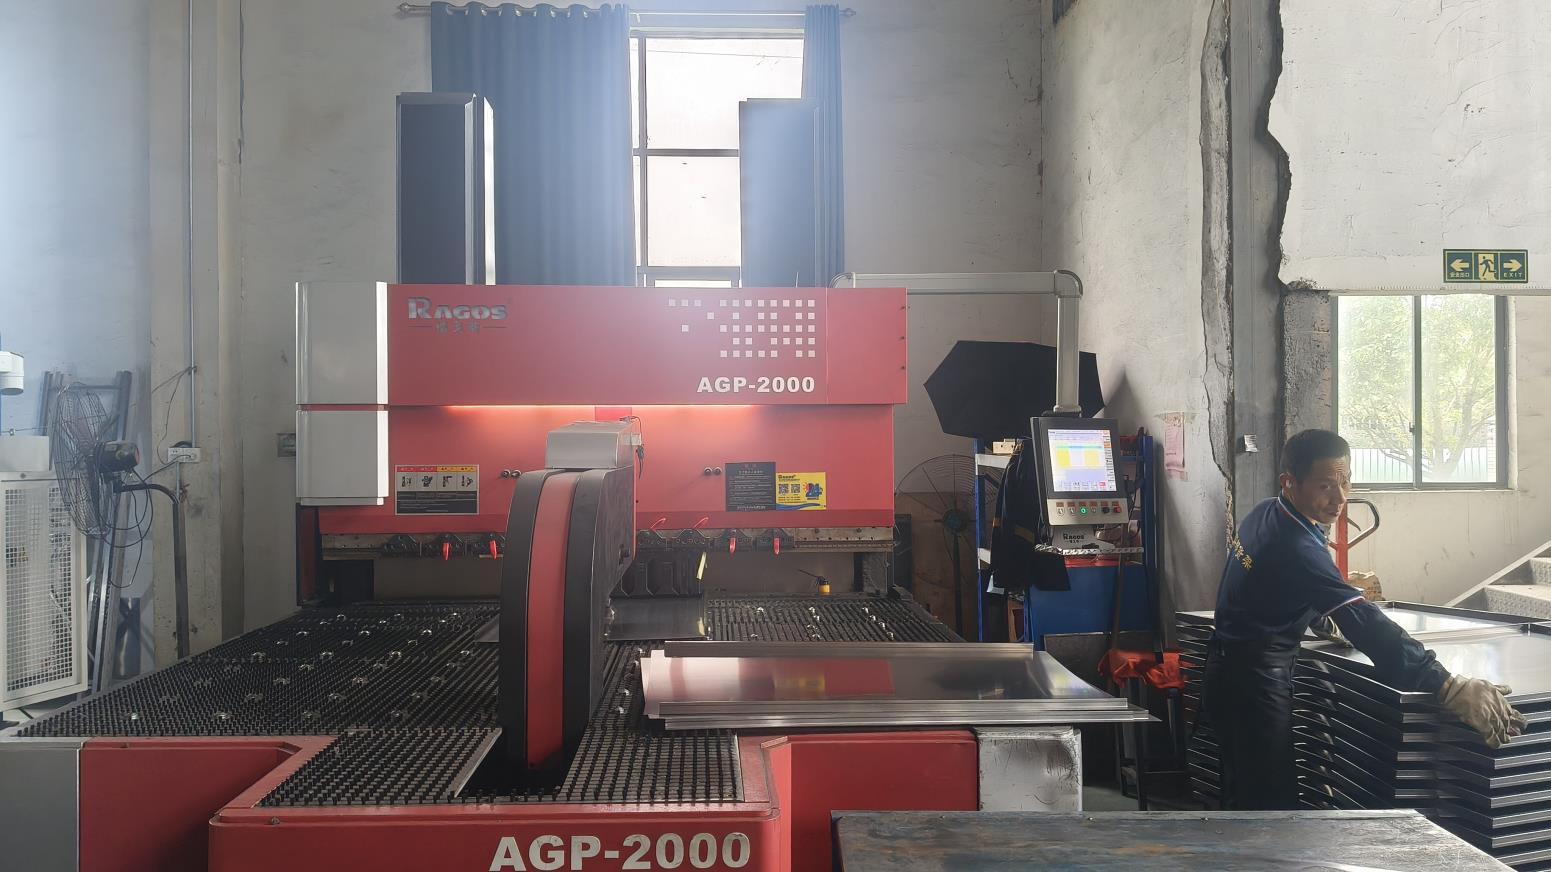
Bending
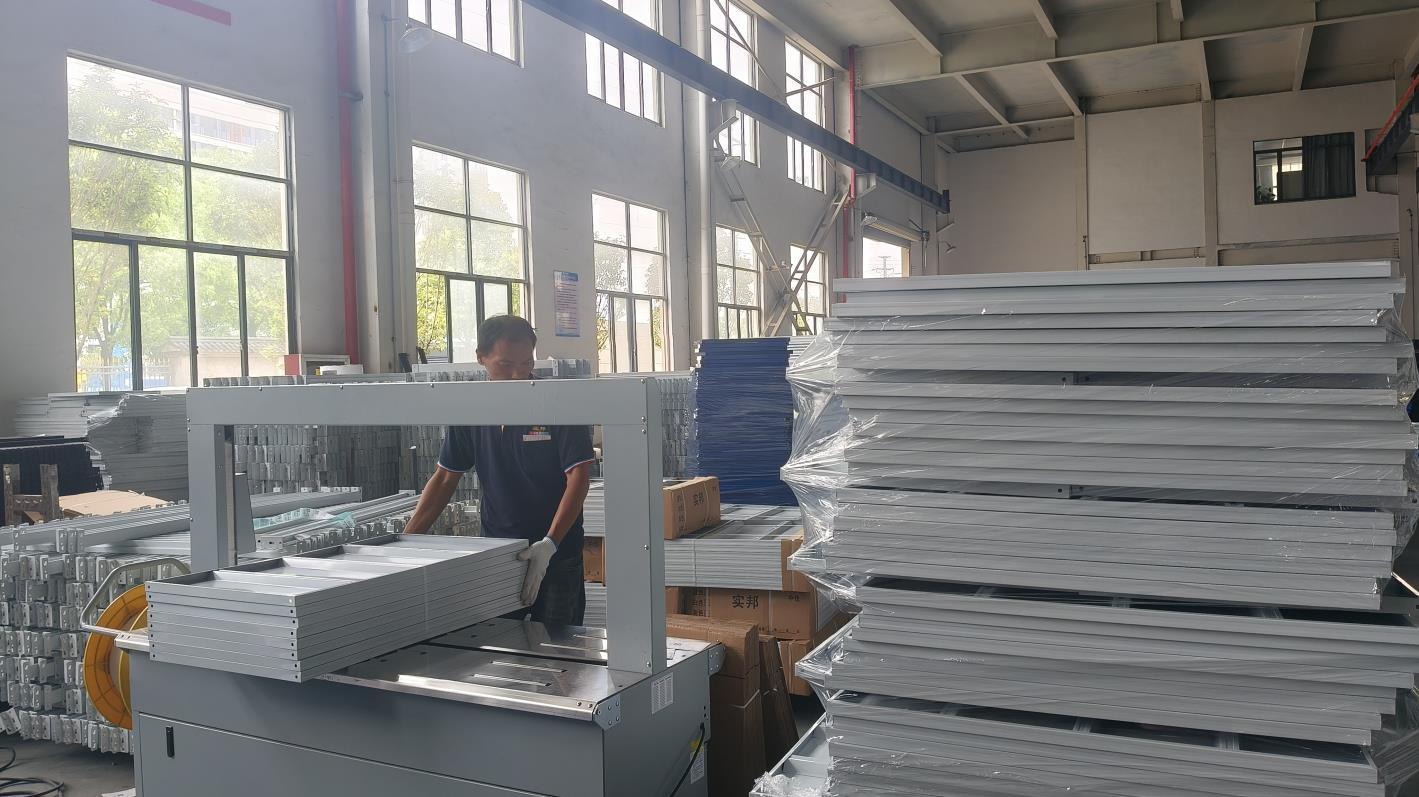
Packaging
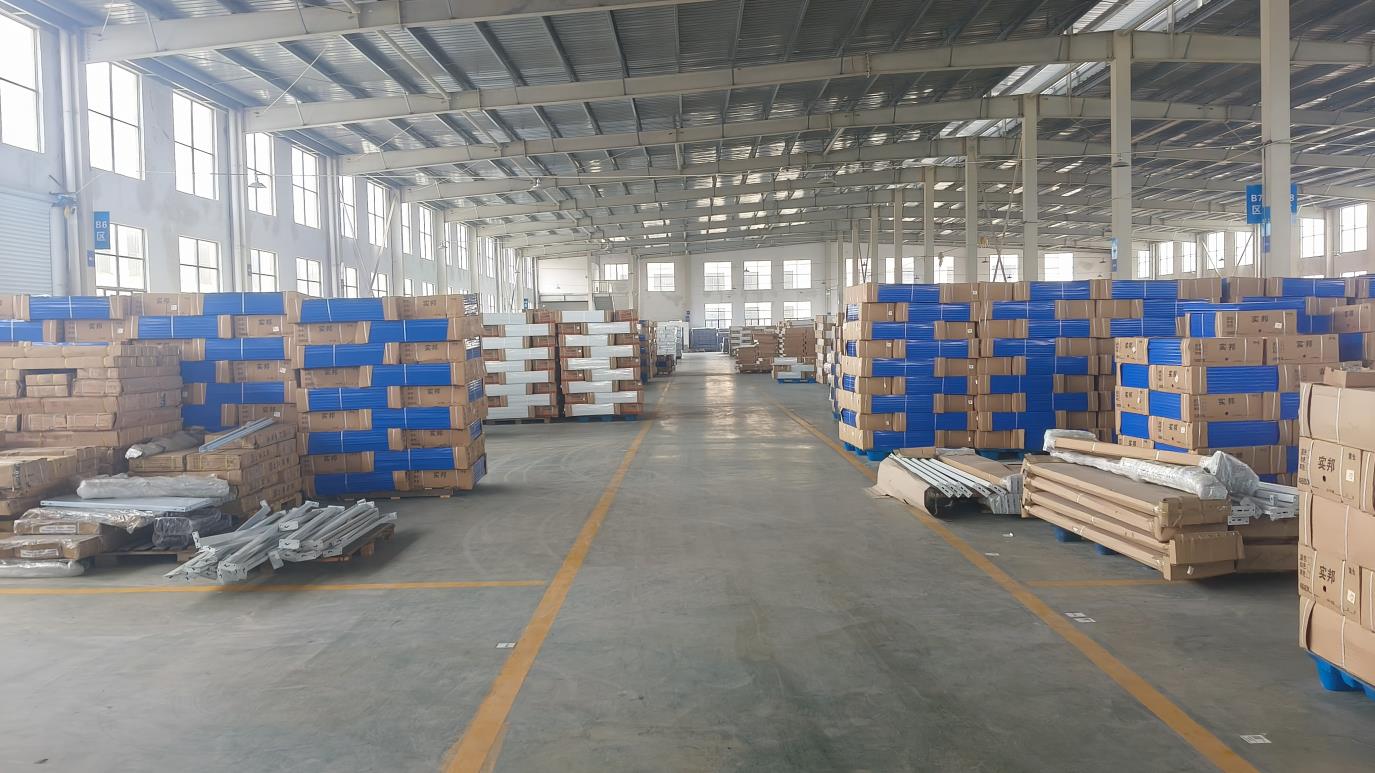
Warehouse
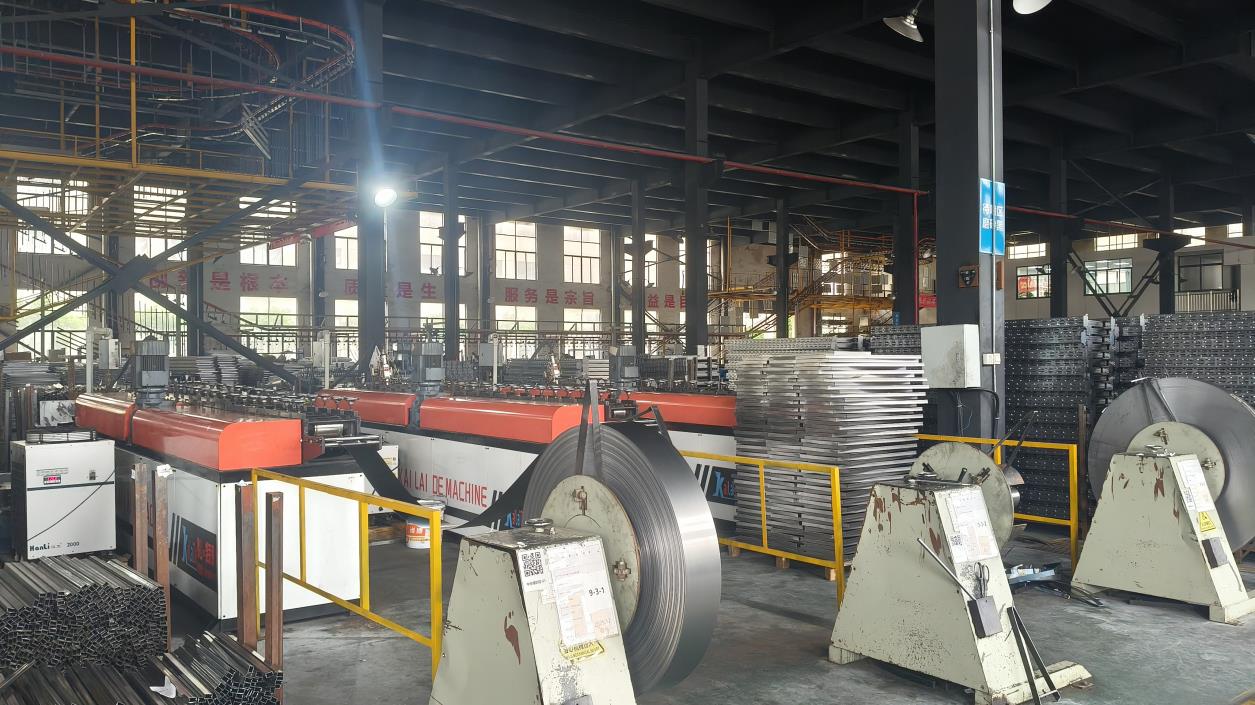
Forming machine
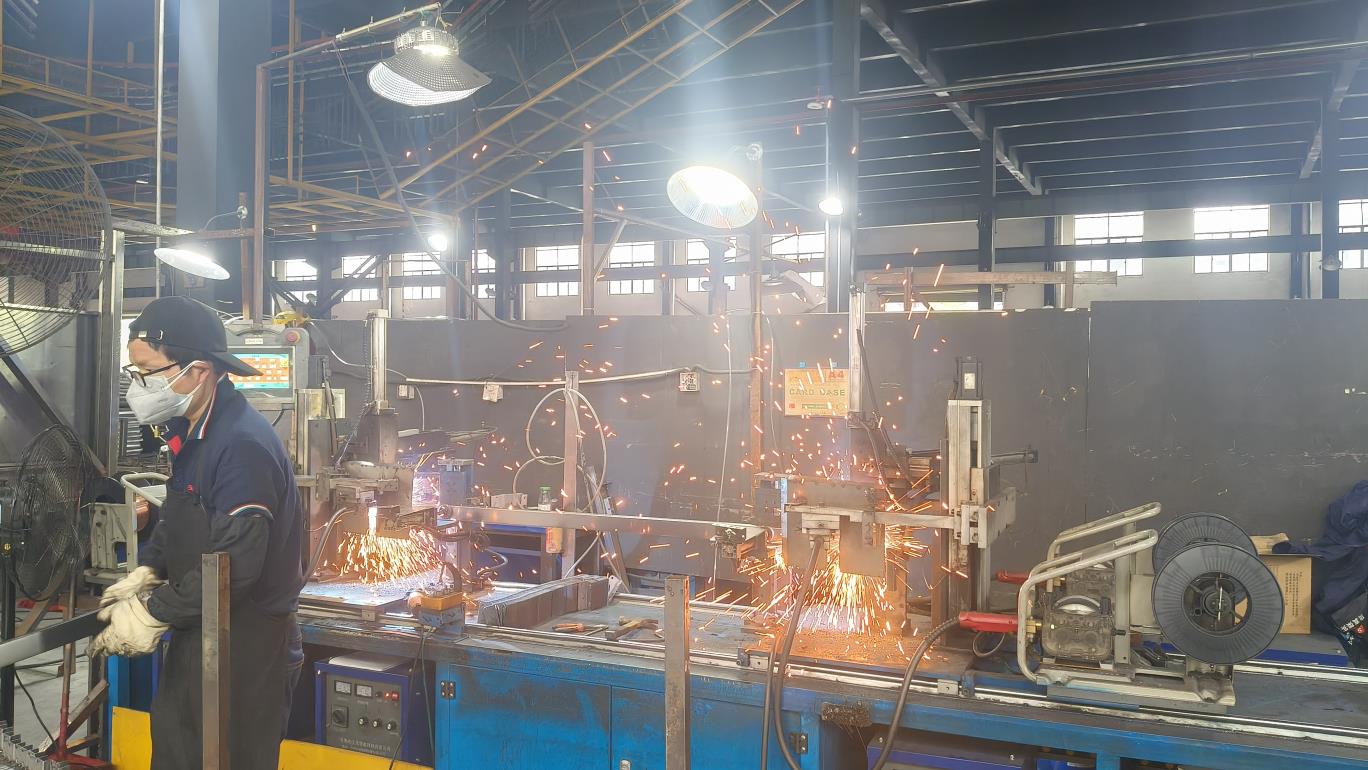
Bonding machine
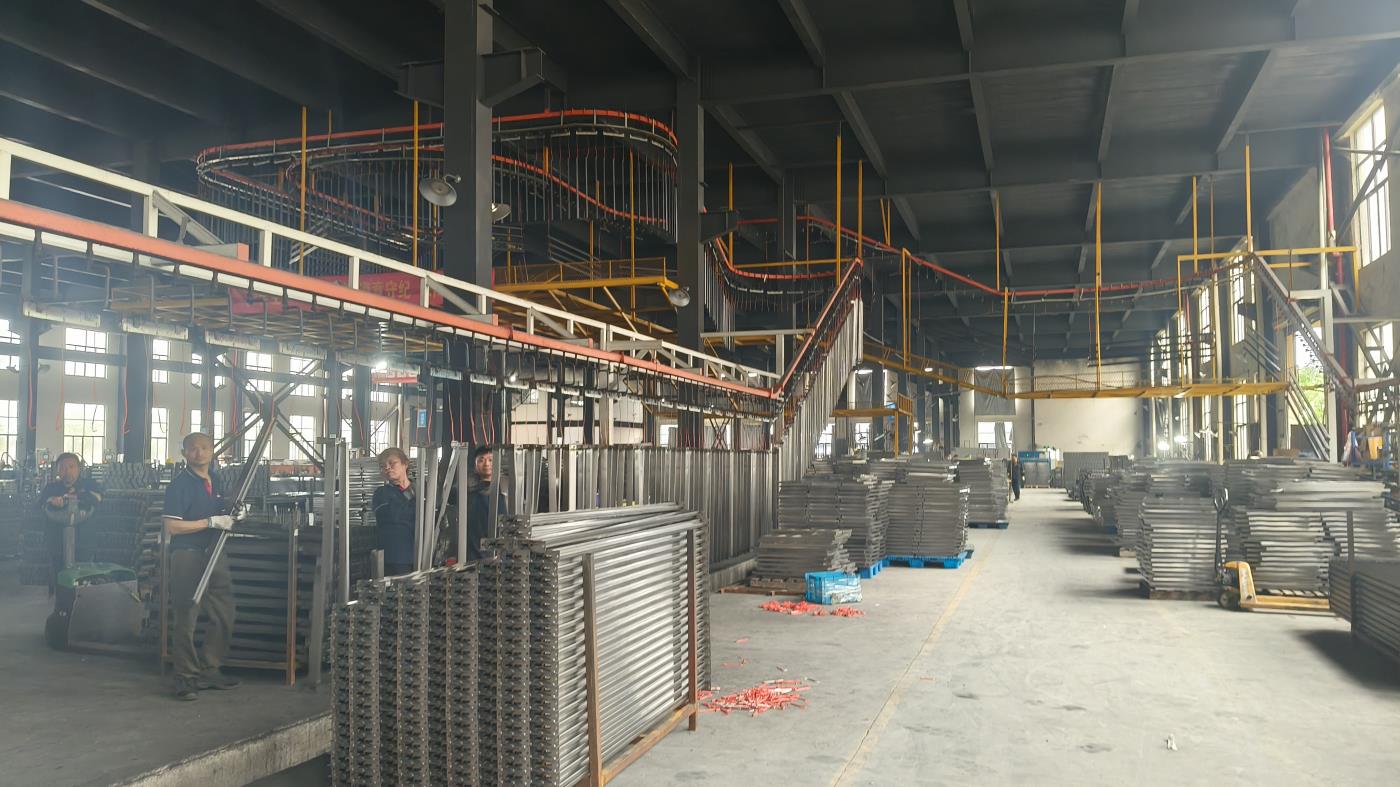
Spray painting line
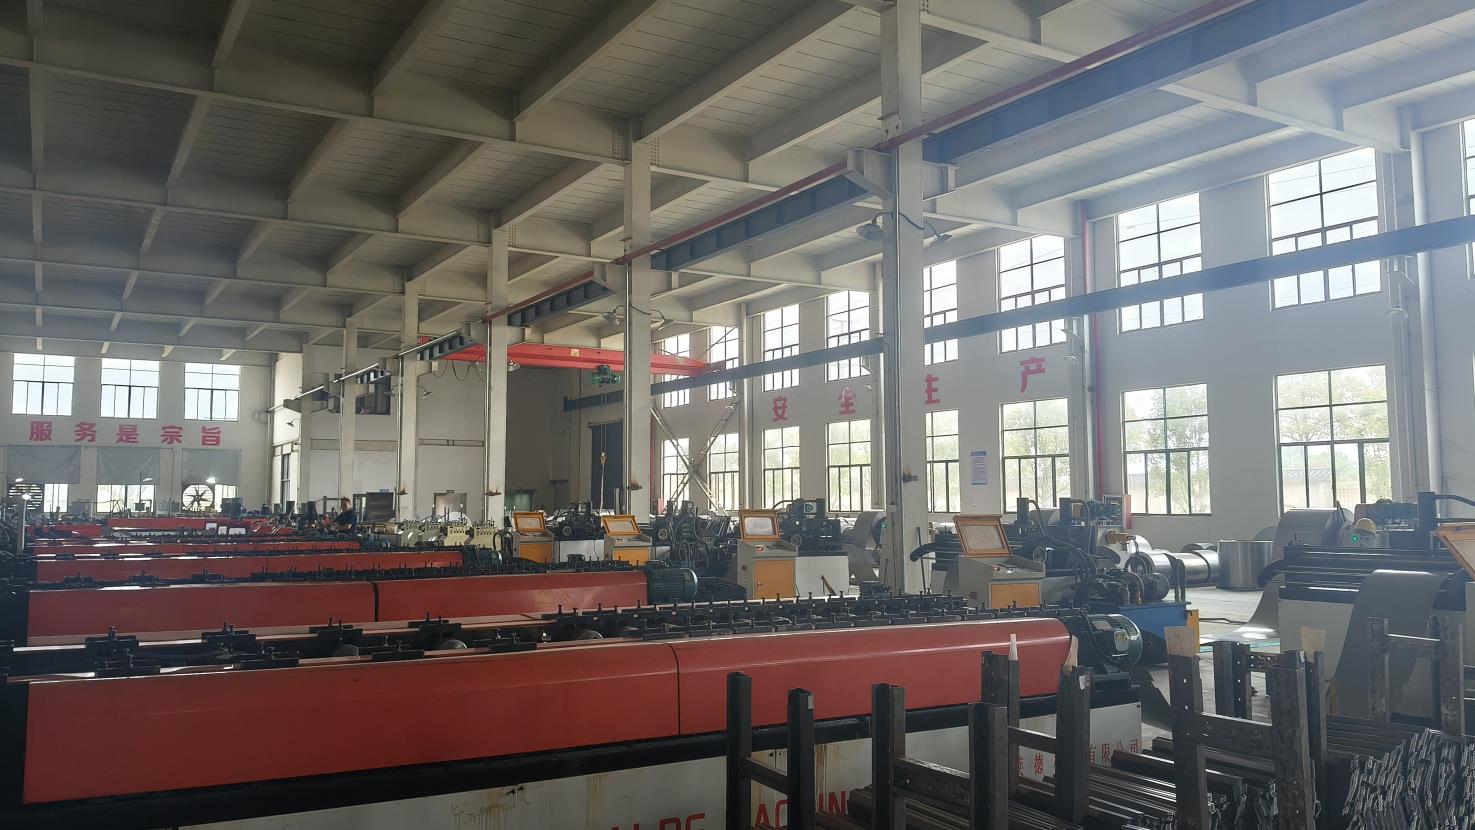
Fully automatic forming machine
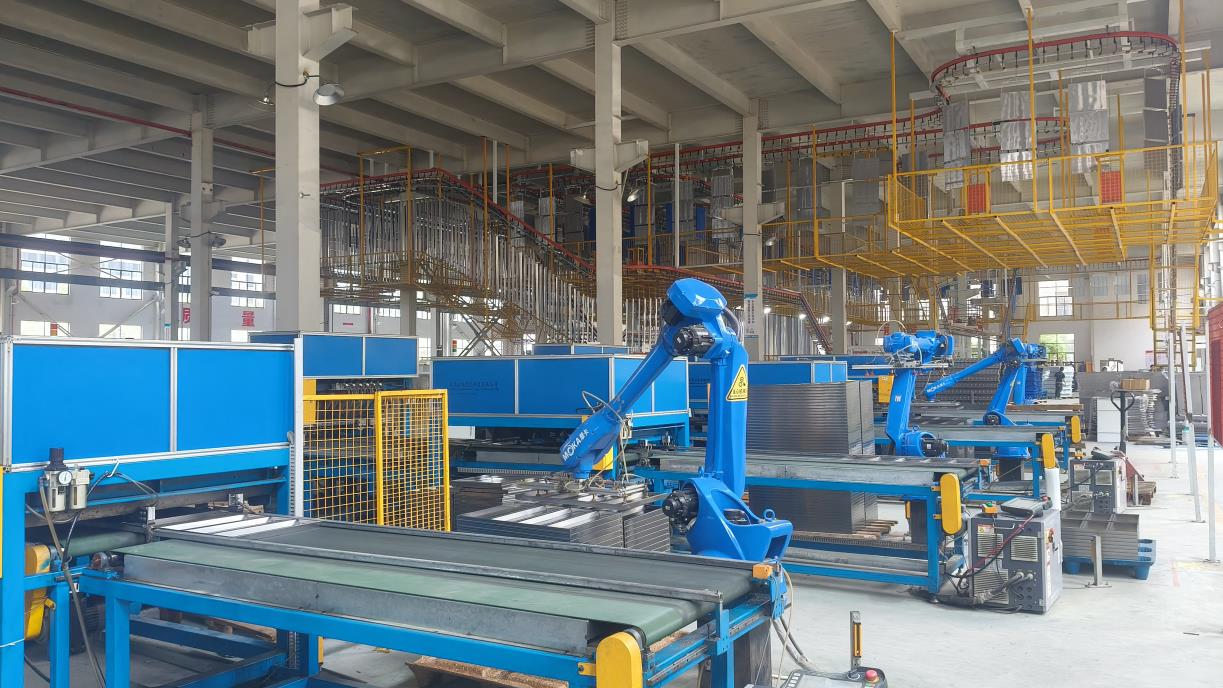
Mechanical arm
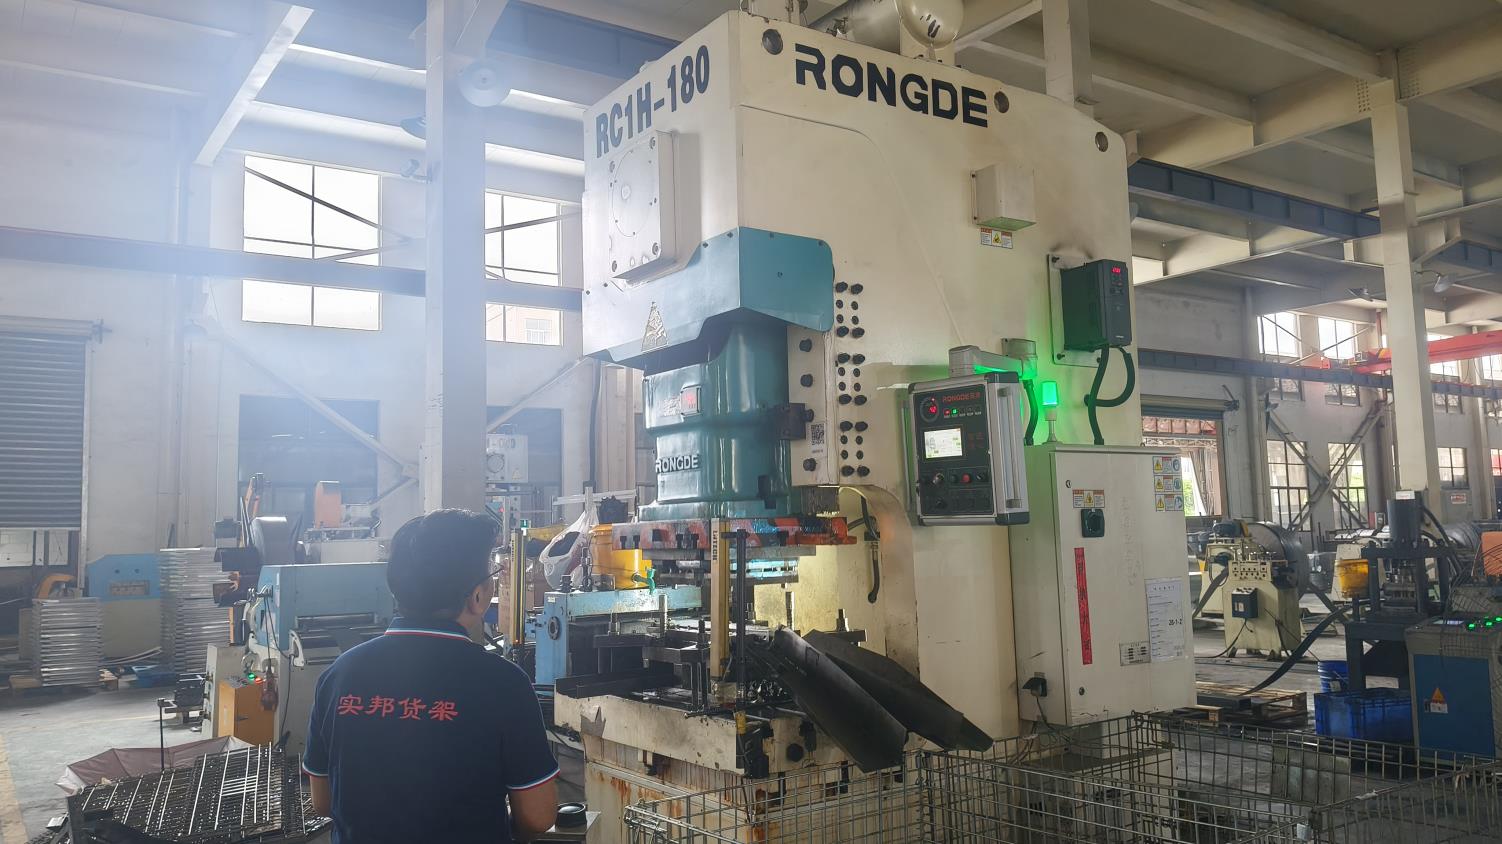
Punching machine
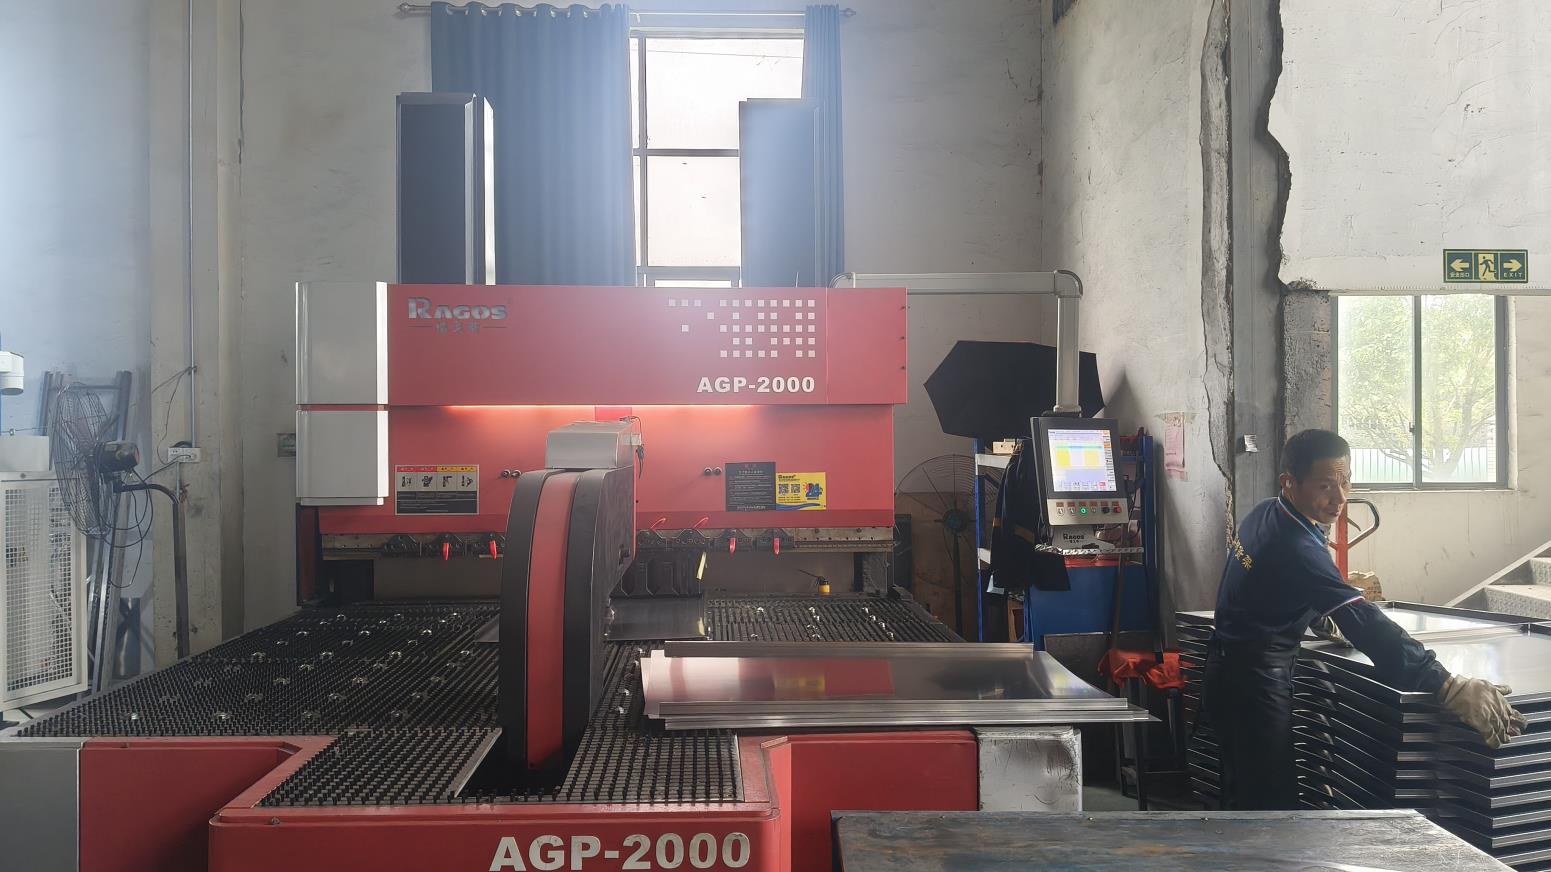
Fully automatic bending machine
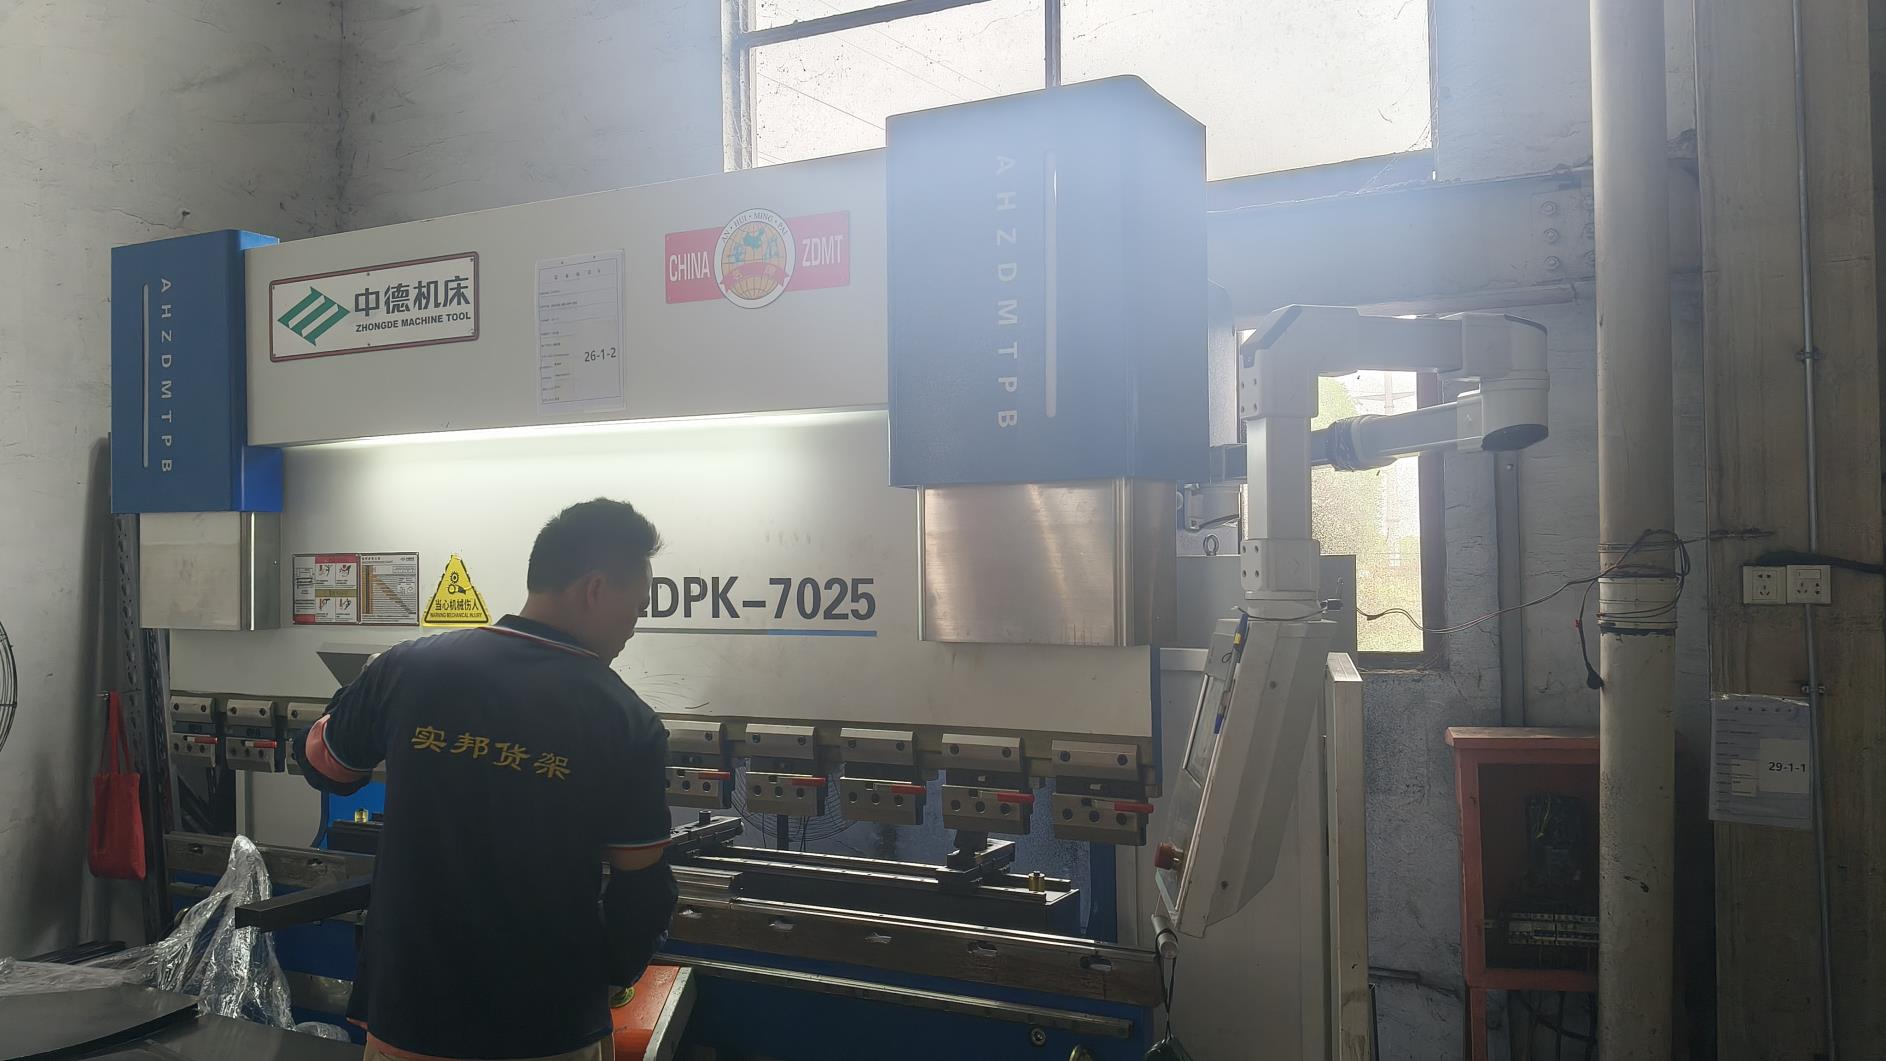
Automatic semi-automatic bending machine
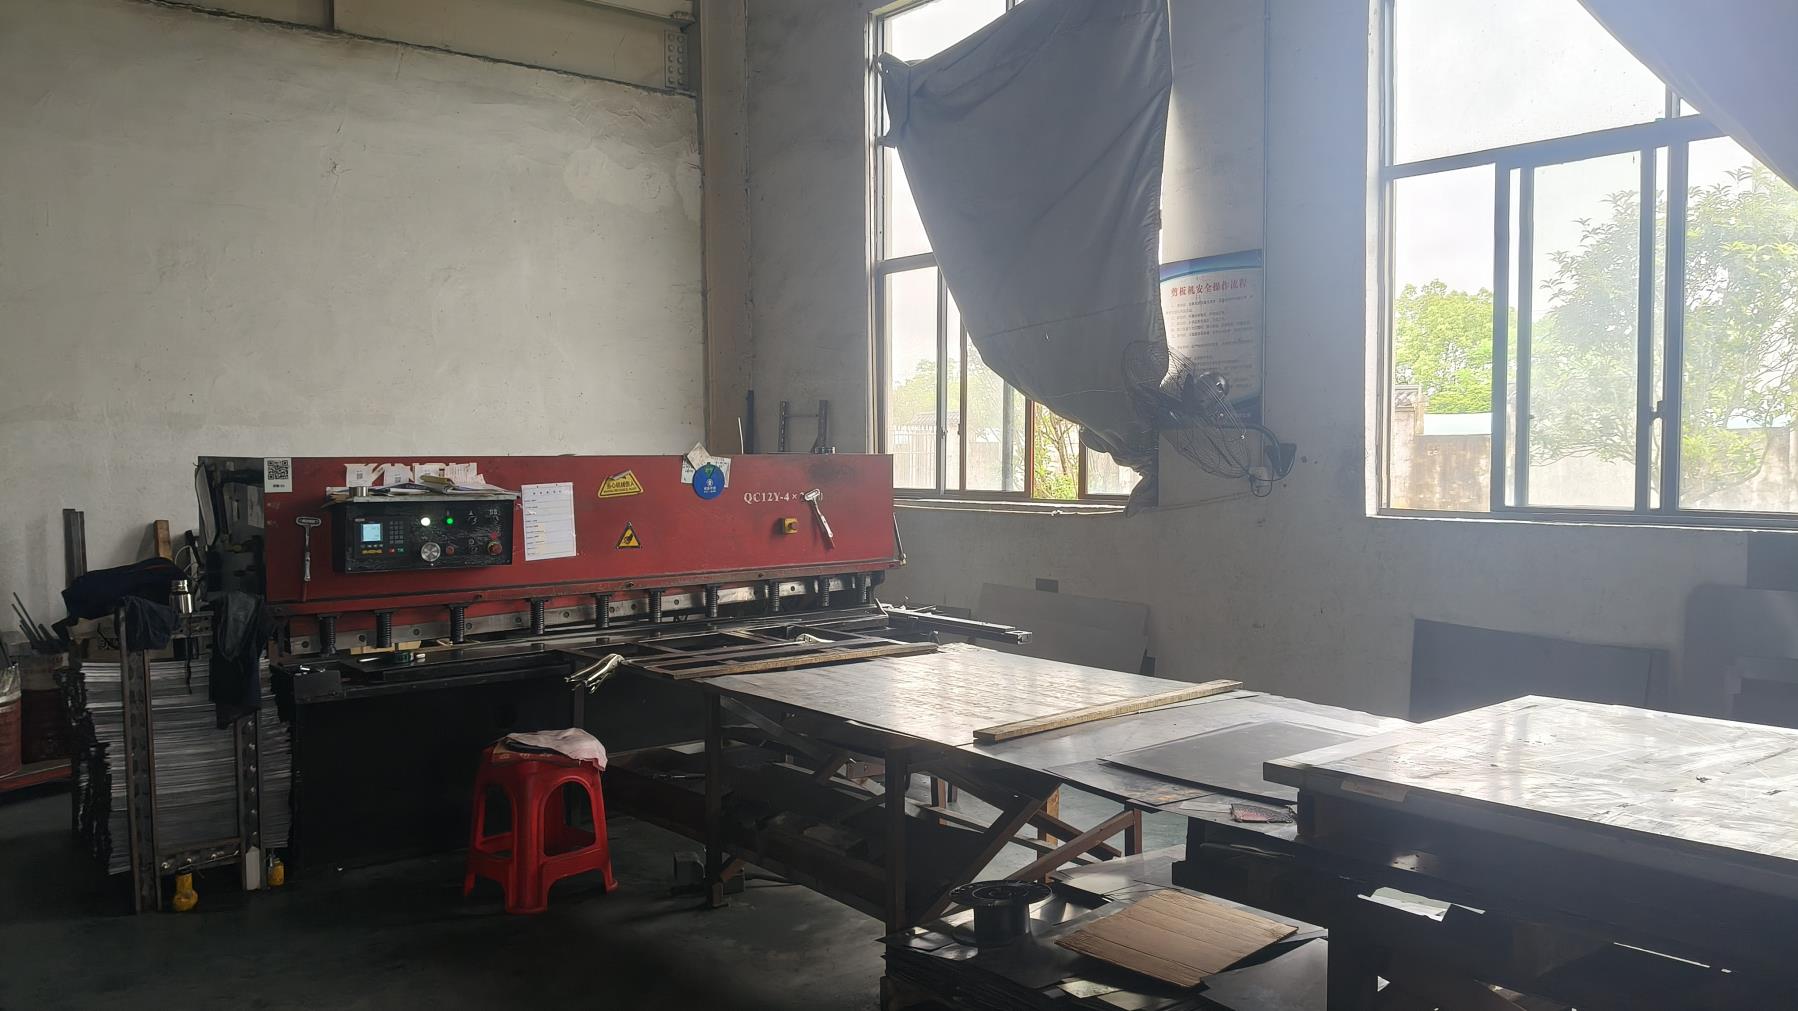
Plate shearing machine
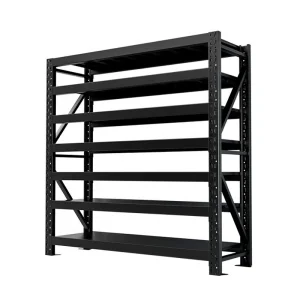
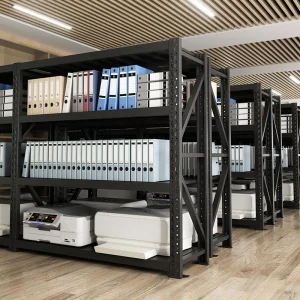
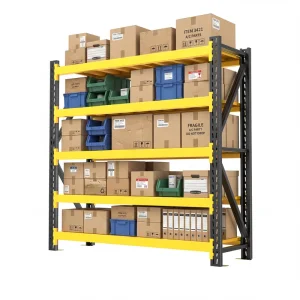
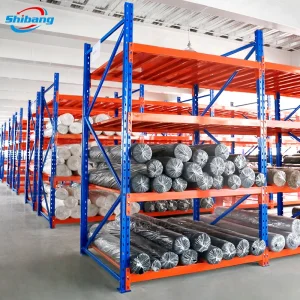
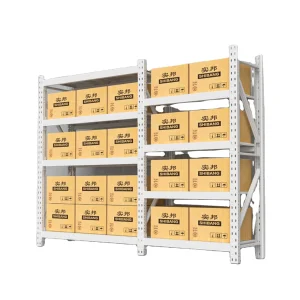
As the global warehousing sector moves towards automated AS/RS (Automated Storage and Retrieval Systems) and IoT-enabled logistics, Ningbo Shibang Storage Rack Co., Ltd. is pioneering next-generation smart racking frameworks. Our R&D roadmap integrates high-tensile structural alloy steel capable of withstanding extreme dynamic loads while maintaining minimal deflection tolerances. By adopting IoT-integrated strain sensors directly within the upright columns, our systems offer real-time structural health monitoring, predictive maintenance alerts, and seamless compatibility with autonomous mobile robots (AMRs) and high-speed stacker cranes.
Modern global enterprises face unprecedented supply chain pressures, requiring storage infrastructure that is both scalable and modular. From cold storage environments operating at -30°C to high-density e-commerce fulfillment centers processing tens of thousands of SKUs daily, our customized heavy-duty rack solutions are designed for macro-level adaptability. We provide comprehensive warehouse layout planning, seismic calculation modeling, and load optimization analytics to ensure maximal cubic utilization and minimum operational downtime.
Navigating international regulatory frameworks is critical for seamless cross-border procurement. Shibang Racking ensures absolute compliance with international structural standards, including CE certifications, RMI (Rack Manufacturers Institute) guidelines, and FEM standards. Our engineering team conducts rigorous wind, seismic, and live-load simulations tailored to specific regional geographic codes across North America, Europe, and Australia, ensuring complete peace of mind for project stakeholders and facility managers.
Anchored in Ningbo’s world-class manufacturing ecosystem, our 32,000 m² "Factory 4.0" facility utilizes fully automated roll-forming lines, robotic welding arms, and computer-controlled powder coating lines. This technological integration eliminates human error, ensures ultra-precise dimensional tolerances, and maintains an unbroken supply chain backed by 850+ vetted raw material vendors. This translates to uncompromised product quality, rapid lead times, and predictable cost stability for our global B2B clients.
 Shibang Rack